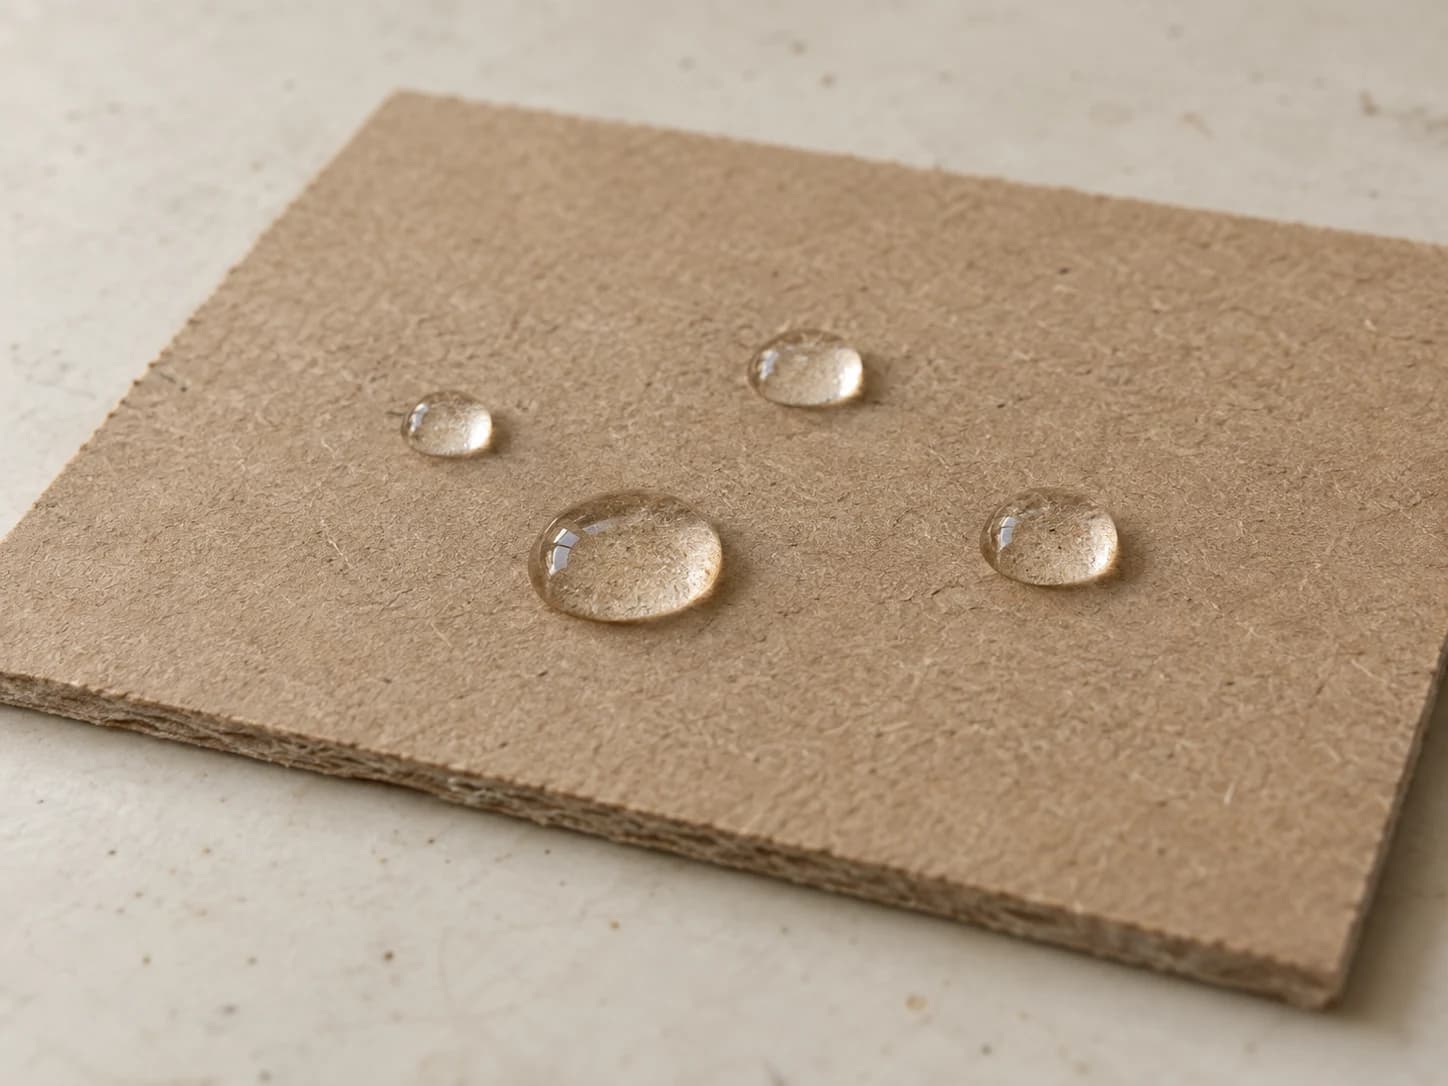
Paper and board that stand up to water
Water-based coatings that protect paper, board and corrugated against liquids and moisture throughout the supply chain.
Designed for recycling and repulping; documentation is confirmed by grade.
Results you can measure in your plant
Reference values from the Michelman technology we represent.
12622–272-min Cobb
Low Cobb, even diluted
HydraBan® keeps Cobb at 22–27 with 80% water in the mix.
90%dilution with water
More coverage per liter
HydraBan® accepts up to 90% dilution with water, lowering cost per coated meter.
0–102-min Cobb
Maximum water resistance
VaporCoat® reaches Cobb values of 0 to 10 for the toughest requirements.
Manufacturer reference values (Michelman). Final performance is confirmed with a trial on your material and line.
What you can do with a water barrier
Turn conventional paper into a water-resistant material without changing your process or recycling route.
Replace plastic laminates
Replace difficult-to-recycle multilayer materials with high-performance, low-environmental-impact barrier solutions.
Customized resistance
Choose the exact level of protection you need based on Cobb values, from adequate to excellent water barrier.
Preserve recyclability
Maintain the recycling, compostability, and repulpability properties of your packaging even with high water resistance.
What you gain with a water-based barrier
Technical performance that fits the processes you already run.
Food contact
Grades with FDA and BfR documentation for food contact, depending on product and use.
Easy application
Compatible with existing Flexography and Rotogravure machines, without the need for special equipment.
High water resistance
Effective protection against liquids with customizable Cobb values according to your barrier needs.
Lower environmental impact
Formulations designed for recycling and repulping; some with PTS results.
Coatings for water barrier
Three series for three levels of demand: from fruit boxes with condensation to packaging that cannot absorb water.
Corrugated board
Boxes for fruits, vegetables, proteins, and refrigerated products requiring resistance to condensation.
Folding cartons and board
Packaging for frozen foods, takeout boxes, burger packaging, and delivery containers.
Lightweight papers
Food wrappers, paper bags, cups and containers for hot and cold drinks, greaseproof paper for baking.
HydraBan® series
Liquid water resistance
- Cobb values 22-28 2 minutes
- Dilutable up to 90% with water
- Water resistance on paper and board
- Check bonding with the chosen adhesive
- Evaluate printing on the coating
Michem® Coat series
Grease and added functionality
- Cobb values 10-20 2 minutes
- Dilutable up to 30% with water
- Oil and grease barrier
- Selected grades add water resistance
- Gluing and other properties depend on grade
VaporCoat® series
Water vapor barrier
- Cobb values 0-10 2 minutes
- Water vapor transmission control
- Grades with water and grease resistance
- Validate closure, especially with water-based adhesives
- Evaluate in the complete structure
2 min Cobb vs. Dilution
HydraBan® series performance
The high dilution of the HydraBan® series makes it cost-effective for applications that need an adequate water barrier.
Economic yield
up to 5 times more effective product at 80% dilution.
Stability
Cobb values go from 22 to 27 even at 80% dilution.
Lower absorption
from an initial Cobb of 126.23 to a 22-27 range.
Flexibility
adjust the concentration to the barrier you need.
Product comparison
| Features | HydraBan® Series | Michem® Coat Series | VaporCoat® Series |
|---|---|---|---|
| Primary function | Liquid water | Oil and grease | Water vapor |
| Cobb Values (2 min) | 22-28 | 10-20 | 0-10 |
| Water Dilutability | Up to 90% - Maximum economic efficiency | Up to 30% | Limited |
| Gluing | Validate with the adhesive | Validate with the adhesive | Validate with the adhesive |
| Printing | Validate with the ink | Validate with the ink | Validate with the ink |
Higher Cobb value = Higher water absorption
Applications of water barriers
Transform your products with waterproofing solutions that maintain the integrity of your packaging in humid conditions
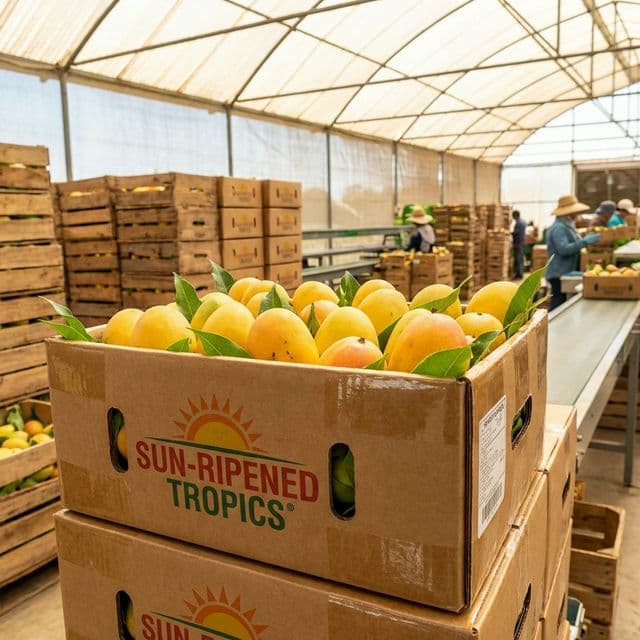
Agricultural boxes
Corrugated board with water barrier to maintain freshness and resist moisture from agricultural products.
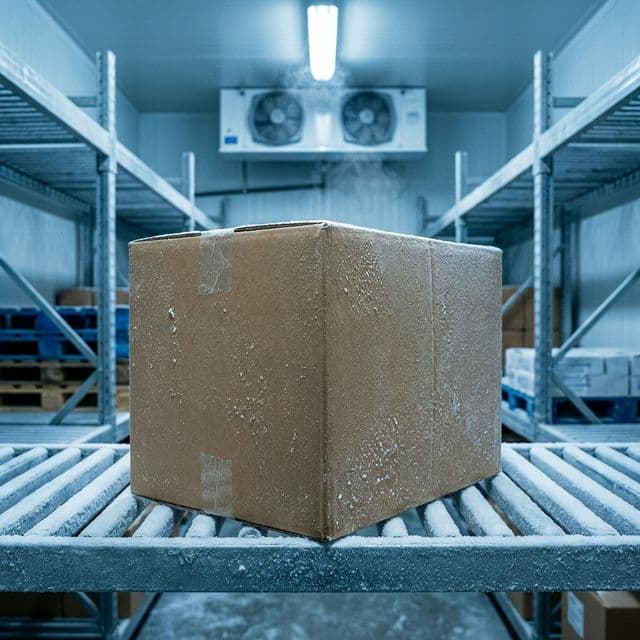
Refrigerated boxes
Packaging for proteins and frozen products that prevent degradation by condensation and moisture.
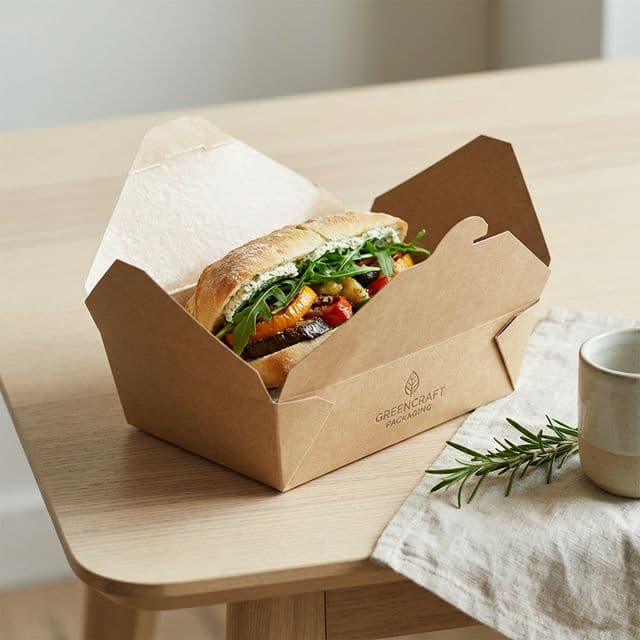
Food packaging
Folding cartons for burgers, wraps, and moist or greasy foods for delivery and restaurants.
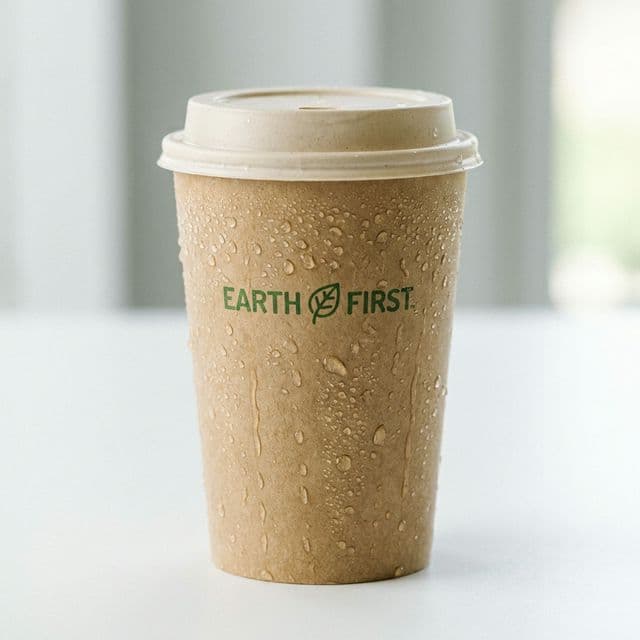
Paper cups
Lightweight papers with coating for hot and cold drinks replacing traditional PE.
Application methods
Our water barrier coatings are compatible with various printing and application systems, facilitating their integration into your existing production processes.
Compatible equipment
Flexographic presses
Adaptable to any varnishing or printing station, offering excellent versatility for in-line application during the printing process. Ideal for cardboards, folding cartons, and medium-weight papers.
Rotogravure
Provides uniform and high-precision coatings in high-volume productions. Allows exact control of coating thickness, optimizing product consumption and improving yield.
Coating units
Independent varnishing units equipped with anilox rollers or transfer systems for off-line applications. Compatible with corrugators for direct application on corrugated board of different calipers.
Application process
Coating preparation
Depending on the selected series, the product can be diluted with water in different proportions to optimize performance and cost:
- HydraBan® Series: Up to 90% dilution with water, maintaining stable Cobb values between 22-27 points
- Michem® Coat Series: Up to 30% dilution with water, ideal for applications requiring higher barrier
- VaporCoat® Series: Limited dilution, for maximum protection against water and grease
Application
- Substrate and coated side
- Trial-defined target dry coat weight
- Coverage uniformity and continuity
For applications requiring higher barrier, consider applying two coats with intermediate drying instead of one thick coat, which improves uniformity and yield.
Drying
Our coatings are compatible with conventional drying systems:
- Hot air: temperature, airflow and residence time
- IR: power, distance and line speed
Validate temperature and time for the grade, substrate and coat weight. Check film formation and avoid damaging the material.
Quality control
Measure absorption using an agreed Cobb protocol and compare with your application target.
- Adequate barrier: Cobb 22-28
- Good barrier: Cobb 10-20
- Excellent barrier: Cobb 0-10
For grease, validate the method with the laboratory and test with actual contents. Kit is not a universal barrier measurement for water-based coatings.
Frequently asked questions
What is the Cobb test and how to interpret its results?
The Cobb test is a standardized method for measuring water absorption in paper and cardboard. It is expressed in g/m² and represents the amount of water absorbed by a sample in a given time (usually 2 minutes). A lower Cobb value indicates better water resistance. For example, a Cobb value of 5 g/m² means excellent water resistance, while a value of 25 g/m² indicates moderate resistance. This measurement is crucial for determining the suitability of the coating for different applications.
Are these coatings suitable for all types of papers and cardboards?
They are formulated for a wide range of cellulosic substrates: corrugated board (200-500 g/m²), folding cartons and board (180-350 g/m²) and lightweight papers (30-120 g/m²). Grade and coat weight are defined by trial for each substrate.
What are the main differences between HydraBan®, Michem® Coat, and VaporCoat® series?
The HydraBan® Series offers an adequate barrier (Cobb 22-28) with high dilutability. The Michem® Coat Series provides a good barrier (Cobb 10-20) with medium dilutability. The VaporCoat® Series provides an excellent barrier (Cobb 0-10) with additional resistance to grease and moisture.
Do the coatings affect the recyclability or compostability of the packaging?
They are designed to keep the package recyclable and repulpable. Results depend on grade, coat weight and structure, and are confirmed with each product’s documentation.
What food safety certifications do these coatings have?
Food contact options are available. Confirm current grade and application documentation for the food, time, temperature and destination market.
What advantages do your coatings offer over traditional plastic laminates?
They remove a plastic layer, run in-line on existing equipment and make the package easier to recycle. The protection level is validated against the laminate they replace.
Find the right coating for your packaging
Complete the technical form and we will send a recommendation for your application.